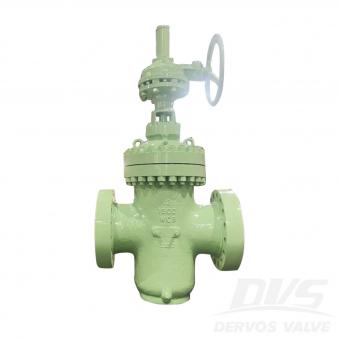
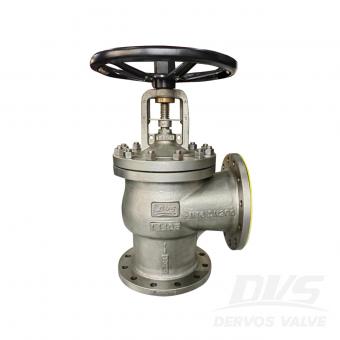
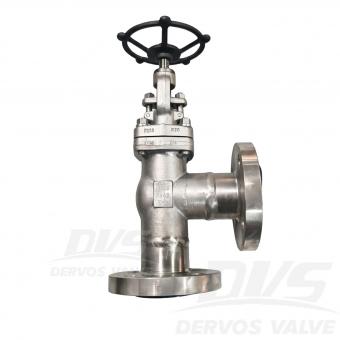
A gate valve that will not open after shutdown may be pressure locked or thermally bound, and the shutdown history usually separates the two. Pressure locking means pressure is trapped in the bonnet cavity; thermal binding means a hot-closed wedge has developed mechanical interference during cooldown. Neither is an automatic reason to raise the actuator torque setting. Pressure Locking Starts in the Bonnet Cavity Pressure locking can affect flexible-wedge and double-disc gate valves when liquid enters the bonnet cavity during operation or through slight seat movement or leakage. Once the valve is closed, that liquid may be trapped between the two seating boundaries. The problem develops when cavity pressure exceeds the pressure on both sides of the closed gate. The line may have been depressurised after the cavity filled at operating pressure, or trapped liquid may have heated and expanded. The resulting load forces the closure element against both seats, leaving normal actuator thrust insufficient to start opening. A failed opening after line depressurisation, or after the closed valve was heated, points toward pressure locking. Where an approved connection permits measurement, bonnet pressure is stronger evidence than high motor current or a torque trip alone. Thermal Binding Follows Hot Closure and Cooldown Thermal binding follows a different sequence. A wedge gate valve is seated hot and the system cools before the next opening command. Unequal contraction of the body and wedge can increase mechanical interference at the seats. Solid wedges are particularly susceptible, although large temperature changes can also affect flexible wedges. This mechanism does not require an overpressurised cavity. Its strongest clue is timing: the valve closes normally at operating temperature but refuses to open after cooldown. Behaviour that changes as temperature returns toward the closing condition supports the diagnosis, but deliberate reheating requires an approved procedure. Uncontrolled external heating is unsafe. Reconstruct the Shutdown Before Touching the Torque Switch Start with the pressure and temperature timeline. Record when the valve closed, whether either side was later drained or depressurised, whether the body remained exposed to heat, and the temperature at the failed opening attempt. Confirm the gate design from drawings or manufacturer records; solid-wedge, flexible-wedge and double-disc designs do not share the same susceptibility. Rule out ordinary faults such as lost power or pressure, wrong limit or torque-switch settings, stem or packing friction, gearbox damage, corrosion and debris. Actuator alarms and the point where movement stopped help distinguish a drive problem from a gate held at the seats. Do not bypass the torque switch or repeatedly hammer the valve open. Extra thrust may bend the stem, damage the seats or overload the gearbox. A larger actuator d...
1. Suzhou Neway Valve Co., Ltd. — NEWAY NEWAY is one of China's most internationally recognized industrial valve manufacturers. Its product range includes ball valves, gate valves, globe valves, check valves, butterfly valves, cryogenic valves, subsea valves, and other engineered valve solutions. The company has strong experience in oil and gas, LNG, petrochemical, offshore, and power applications. Best suited for: large-scale energy projects and severe-service applications. 2. CNNC Sufa Technology Industry Co., Ltd. CNNC SUFA is well known for its experience in nuclear power and other high-integrity industrial applications. The company has strong capabilities in material traceability, engineering control, testing, and specialized valve manufacturing. Its products are also used in petroleum, petrochemical, power, and chemical industries. Best suited for: nuclear power, high-integrity systems, and technically demanding projects. 3. DERVOS VALVE DERVOS VALVE supplies industrial valves to customers in oil and gas, petrochemical, power generation, water treatment, marine, and general industrial applications. Its main products include ball valves, gate valves, globe valves, check valves, butterfly valves, plug valves, knife gate valves, line blind valves, and strainers. DERVOS supports international standards such as API, ASME, EN, and DIN, and can provide carbon steel, stainless steel, alloy steel, duplex stainless steel, low-temperature steel, and other materials. One of its key strengths is flexibility. DERVOS can support mixed valve packages, small-to-medium quantities, customized specifications, and project-specific documentation. Best suited for: overseas distributors, EPC projects, customized valves, mixed orders, and flexible sourcing requirements. 4. Yuanda Valve Group Yuanda Valve Group is one of China's large-scale valve manufacturers with broad production capacity. Its product range includes gate valves, globe valves, check valves, butterfly valves, ball valves, and other general industrial valves. The company is widely involved in water supply, HVAC, municipal infrastructure, power, and industrial pipeline projects. Best suited for: large-volume standardized valve procurement and general industrial applications. 5. Jiangsu Shentong Valve Co., Ltd. Jiangsu Shentong focuses strongly on specialized valve applications in metallurgy, energy, nuclear power, and chemical industries. Its strength lies in engineered products for demanding operating conditions rather than only standard valve production. Best suited for: metallurgy, energy, chemical processing, and specialized industrial applications. 6. Chaoda Valves Group Co., Ltd. Chaoda Valves Group serves petroleum, chemical, natural gas, power, and other process industries. Its product range includes ball valves, gate valves, globe valves, check valves, butterfly valves, and special-purpose industrial valves. The company has experience with corro...
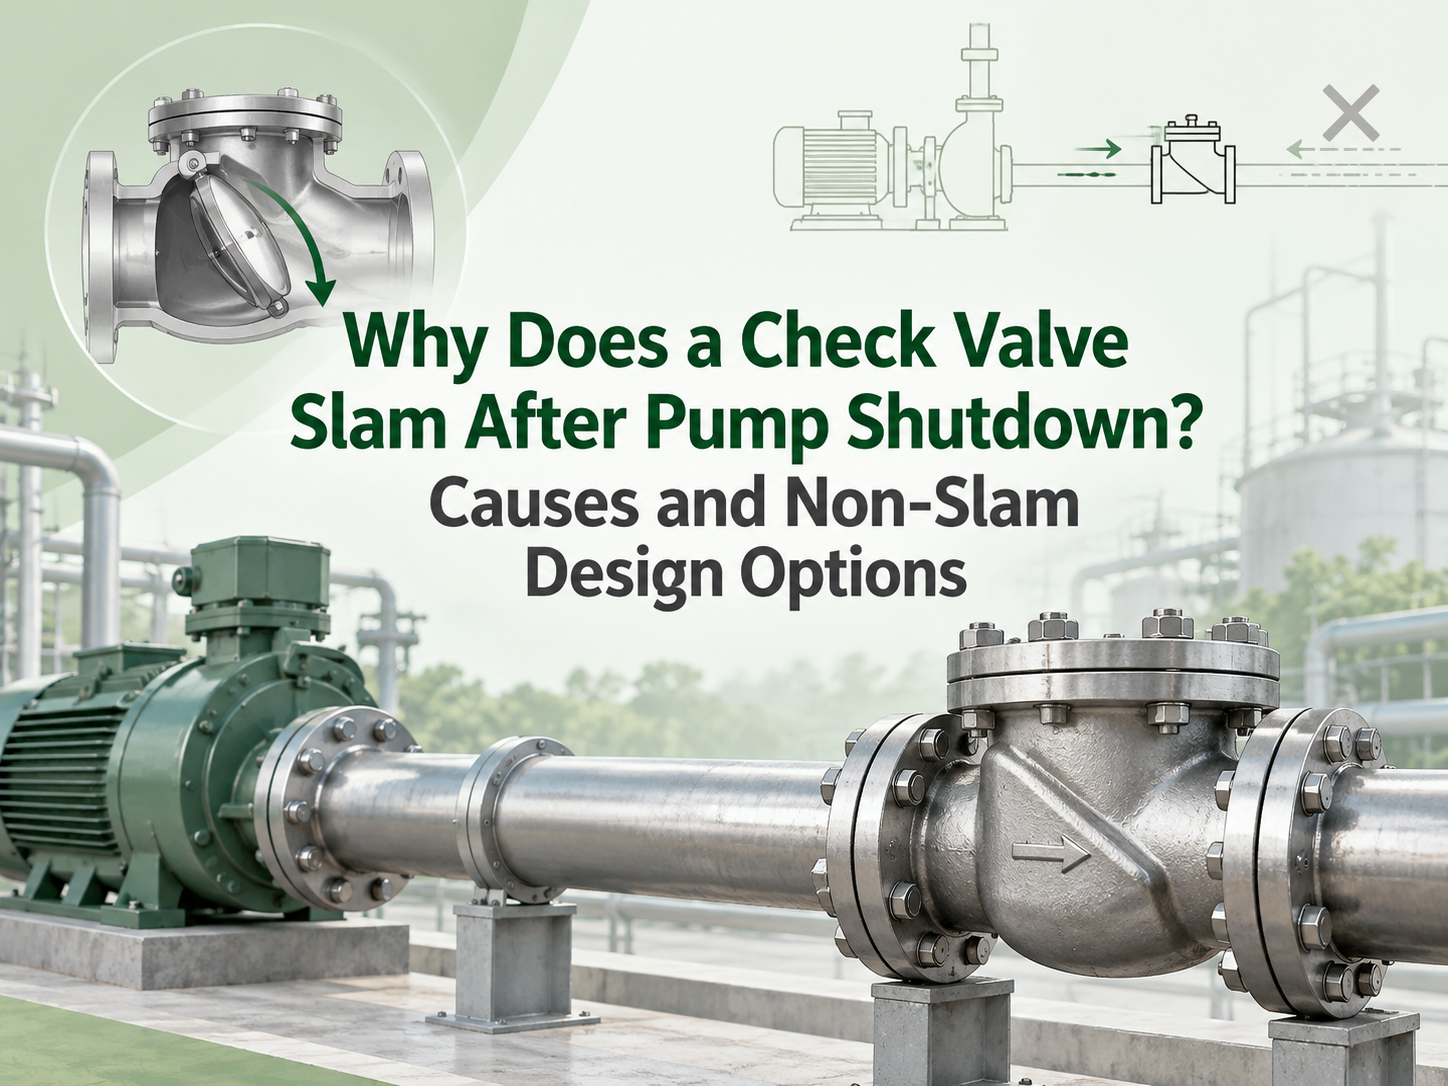
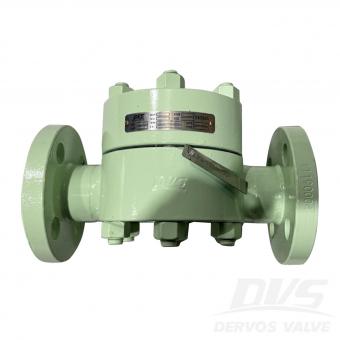
A check valve slams after pump shutdown when flow reverses before the closure member reaches its seat. The valve then stops that reverse velocity abruptly, creating a pressure wave through the piping. The damaging event is usually the rapid arrest of the liquid column, not simply the disc hitting the seat. A “non-slam” label alone is not a solution; the valve response must suit the system's flow deceleration. The Valve Is Closing Too Late for the Shutdown Transient When pump torque disappears, forward velocity falls. Static head, a pressurised common header or another running pump may then drive liquid back toward the stopped pump. If inertia and hinge friction keep a conventional swing disc open through zero flow, reverse velocity develops before the disc reaches its seat. High static lift, a steep rising main, short pump coast-down, parallel pumps and high initial velocity can accelerate this reversal. A long-stroke or high-inertia valve is more likely to lag. This is why the same valve may run quietly in one system and slam in another: nominal size and pressure class do not define shutdown behaviour. Confirm the Event Before Changing the Valve A single hard bang after shutdown points toward check-valve closure or another surge event. Continuous clicking during forward flow is chatter, which more often indicates unstable partial opening, pulsation or poor hydraulic sizing. Record the stop command, motor speed decay, flow direction and pressures on both sides of the valve on a common time base. A high-speed video of an external lever or position indicator can help show when the valve closes. For consequential systems, fast pressure logging is more reliable than sound alone. Inspect the hinge, shaft, spring and seat for friction, wear, deposits or damage, and verify the permitted installation orientation. Check pipe supports as well; the pressure wave may produce its loudest noise away from the valve. Non-Slam Designs Use Different Closing Strategies An axial-flow or nozzle check valve uses a light, centrally guided disc, short travel and spring assistance. It begins closing as forward flow falls, ideally seating before appreciable reversal. It is a strong candidate for rapid pump trips, but pressure loss, cracking pressure, minimum stable flow, orientation and tolerance of solids still matter. A spring-assisted dual-plate valve uses two lighter plates and shorter travel than a conventional swing disc. Its compact construction can improve response, but “dual plate” does not mean slam-free. Plate inertia, spring torque, size and mounting position remain relevant. Tilting-disc, resilient-hinge and spring-assisted swing designs reduce travel or assist closure while retaining a relatively open flow path. They can suit large water lines where energy loss matters, provided dynamic data supports the selected design and size. Large pumping mains ma...
в дополнение к обычным типам клапанов, дерво может также предоставлять некоторые специальные клапаны, такие как игольчатый клапан, предохранительный клапан, регулирующий клапан, поплавковый клапан и так далее.


Авторское право © 2015-2026 DERVOS VALVE CO.,LTD.Все права защищены Блог / Карта сайта / XML / политика конфиденциальности